Stainless steel is chosen because it resists corrosion and keeps a clean appearance, but its surface can still be damaged by the wrong abrasive. Carbon steel contamination, uneven scratch patterns, excessive heat, embedded particles and uncontrolled roughness can all reduce the final quality of the part. For buyers working with stainless steel sheets, welded components, tanks, kitchen equipment, valves, architectural panels or precision parts, abrasive selection is not only about cutting speed. It is also about surface cleanliness, repeatability and downstream process safety.
White fused alumina is a practical abrasive for stainless steel surface finishing when the process requires a hard, sharp and clean mineral abrasive. It can be used for blasting, matte finishing, deburring, weld cleaning, coating preparation and controlled surface texturing. Compared with brown fused alumina, white fused alumina has higher purity and lower iron contamination risk, which is important when the stainless steel surface must remain bright and free from dark metallic residue.
What Is White Fused Alumina?
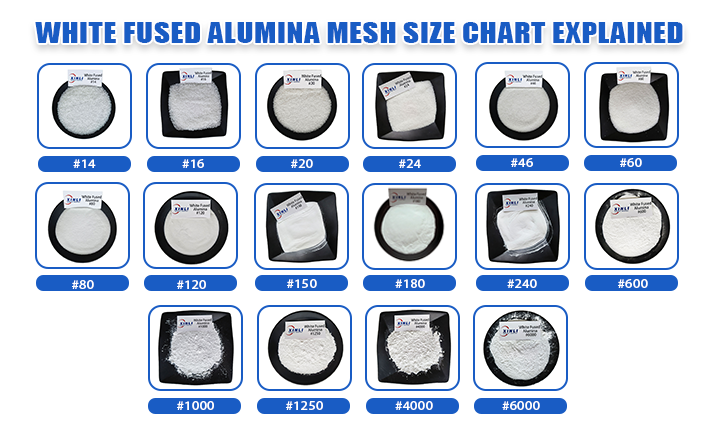
White fused alumina, also called WFA, white aluminum oxide or white corundum, is produced by melting high-purity alumina in an electric arc furnace. After cooling, crushing, magnetic separation and screening, it becomes angular abrasive grains or powders in different standards such as FEPA F grit, FEPA P grit, JIS powder and micron powder.
For stainless steel finishing, buyers usually focus on WFA grit rather than micron powder. The key purchasing points are particle size, shape, magnetic content, dust level, cleanliness, reusability and whether the supplier can keep the same surface result from batch to batch.
Why WFA Works Well on Stainless Steel
- Low iron contamination risk helps protect stainless steel from dark marks and surface pollution.
- High hardness gives strong cutting action for oxide removal, deburring and surface texturing.
- Angular particles create a clear surface profile for coating, painting or bonding processes.
- Clean white color makes it easier to monitor surface cleanliness during precision finishing.
- Stable grading helps control roughness, satin texture and repeatable production results.
Recommended WFA Grit Sizes for Stainless Steel
The correct grit size depends on the starting surface, the required finish and the next process. Coarse grit removes weld discoloration, scale and heavy contamination faster, but it leaves a more aggressive profile. Fine grit produces a smoother matte or satin finish, but it removes material more slowly. Buyers should test on real stainless steel samples before fixing a production specification.
| Stainless steel process | Common WFA size | Practical result |
| Heavy cleaning and rough profile | F36-F60 | Fast removal of oxide, scale or old coating. Use carefully on thin stainless steel to avoid over-roughening. |
| General blasting and coating preparation | F60-F100 | Balanced cleaning speed and surface profile. A useful starting range for coating adhesion trials. |
| Satin or matte surface finishing | F100-F150 | More controlled texture for visible stainless steel surfaces, panels and equipment parts. |
| Fine finishing and light deburring | F150-F220 | Lower impact and finer scratch pattern for precision components and thin parts. |
| Very fine finishing or lapping | 240 mesh, 325 mesh or micron grades | Used only when the process moves beyond blasting into slurry finishing, lapping or polishing support. |
How to Choose by Application
Coating Preparation Before Painting or Bonding
For stainless steel coating preparation, the surface must be clean enough for adhesion but not over-blasted. Many buyers start with F60, F80 or F100 and then check roughness, coating thickness and adhesion results. If the coating is thin, a finer grade may be needed to avoid a profile that shows through the coating.
Visible Satin or Matte Stainless Steel Finish
When the final surface will remain visible, the abrasive should create an even texture without random deep scratches. F100-F150 is often a practical trial range. The buyer should control blasting pressure, nozzle distance, media flow and part movement because the same grit can create different results under different operating conditions.
Deburring and Edge Conditioning
For stainless steel stamped parts, machined parts or laser-cut edges, WFA can remove light burrs and sharpened edges. F120-F220 is often tested when the part is thin or the edge must remain accurate. Coarser sizes may remove burrs faster but can change part geometry if the pressure is too high.
Weld Cleaning and Heat Tint Removal
Welded stainless steel may require cleaning before passivation, coating, or assembly. F60-F100 can be used to inspect weld discoloration and localized oxide removal. Buyers should avoid mixing blasting media that have previously come into contact with carbon steel, as reused contaminated media can transfer iron to the stainless steel surface.
WFA vs Other Media for Stainless Steel
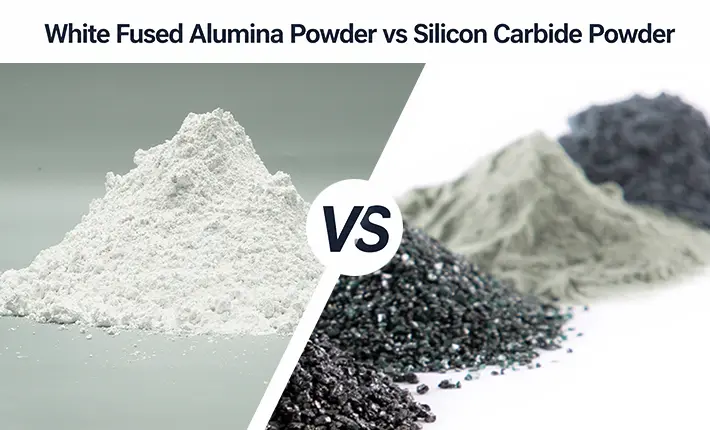
Glass beads can create a softer shot peening effect, but they are slower at removing heavy impurities and cannot create a sharp, anchored profile like white fused alumina. Brown fused alumina is strong and affordable, but carries a higher risk of impurities and color contamination for clean stainless steel machining. Silicon carbide has strong cutting power, but its sharpness may be too high or its cost too expensive for general stainless steel finishing. White fused alumina is typically chosen when buyers require a clean, sharp, and easily controllable abrasive for stainless steel machining.
FAQ
Is white fused alumina safe for stainless steel surface finishing?
Yes, it is commonly used when a clean, hard and low-iron abrasive is needed. The media and equipment must be kept free from carbon steel contamination.
Which grit size should I test first for stainless steel blasting?
For coating preparation, F60-F100 is a practical starting range. For visible matte finishing, F100-F150 is often more suitable.
Can WFA remove weld discoloration on stainless steel?
It can help remove oxide and heat tint, but the final process should be tested with the actual weld condition and any passivation requirement.
Is WFA better than glass beads?
It depends on the finish. Glass beads give a softer peened look, while WFA cuts faster and creates a sharper surface profile.